Tubular Chain Conveyors
Overview
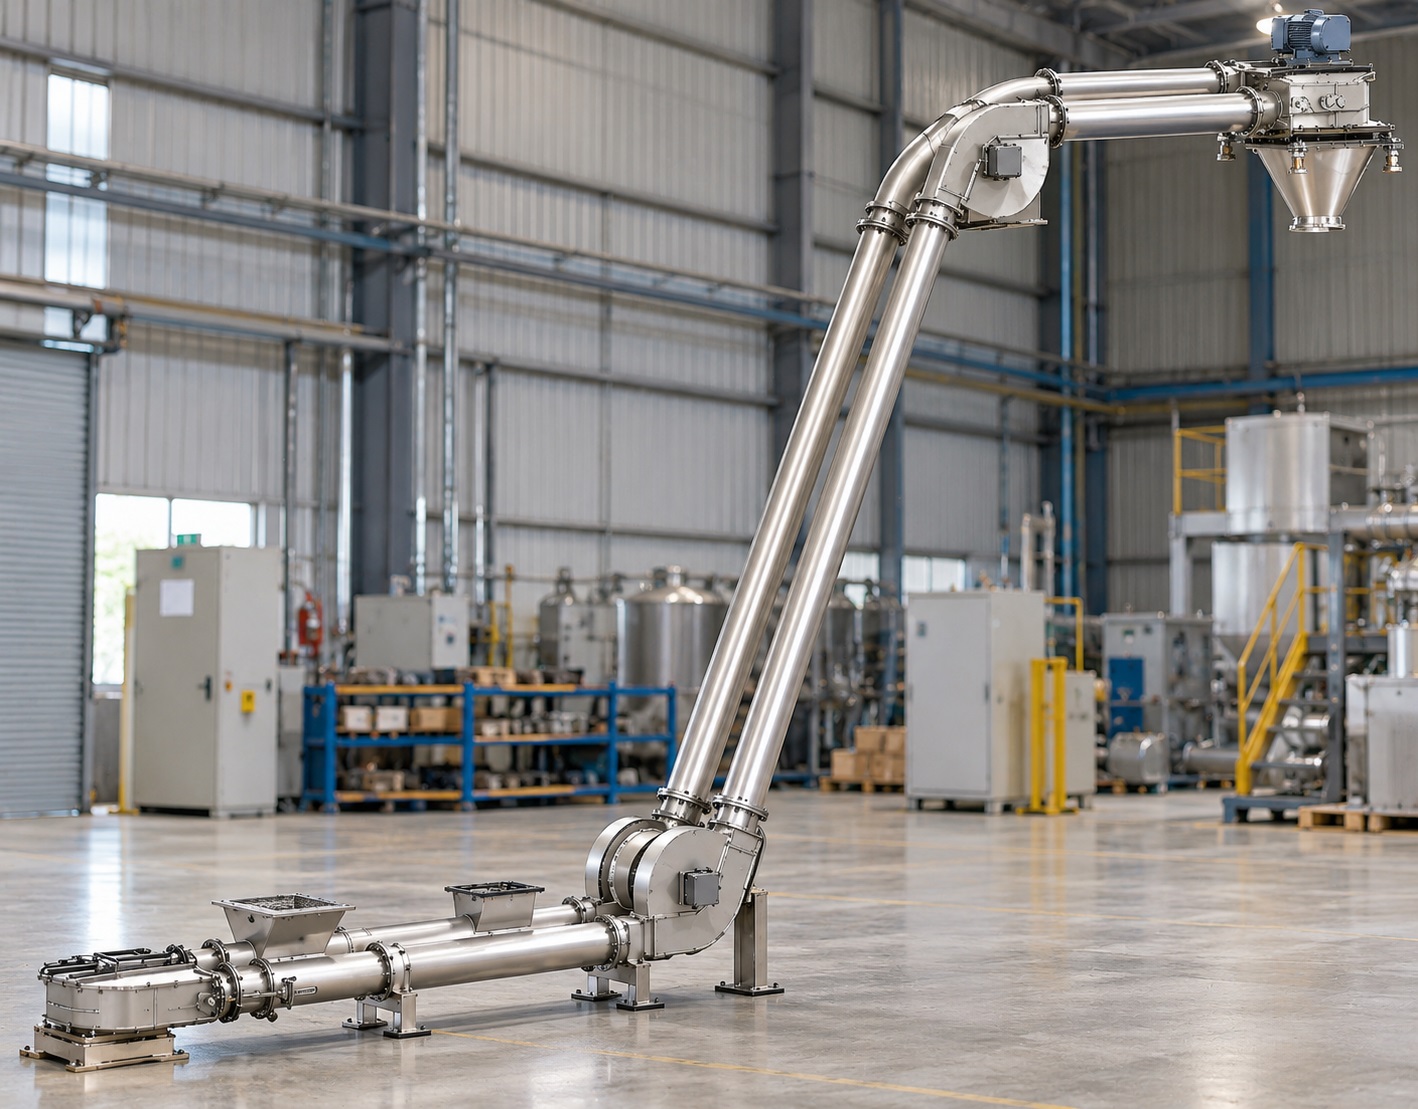
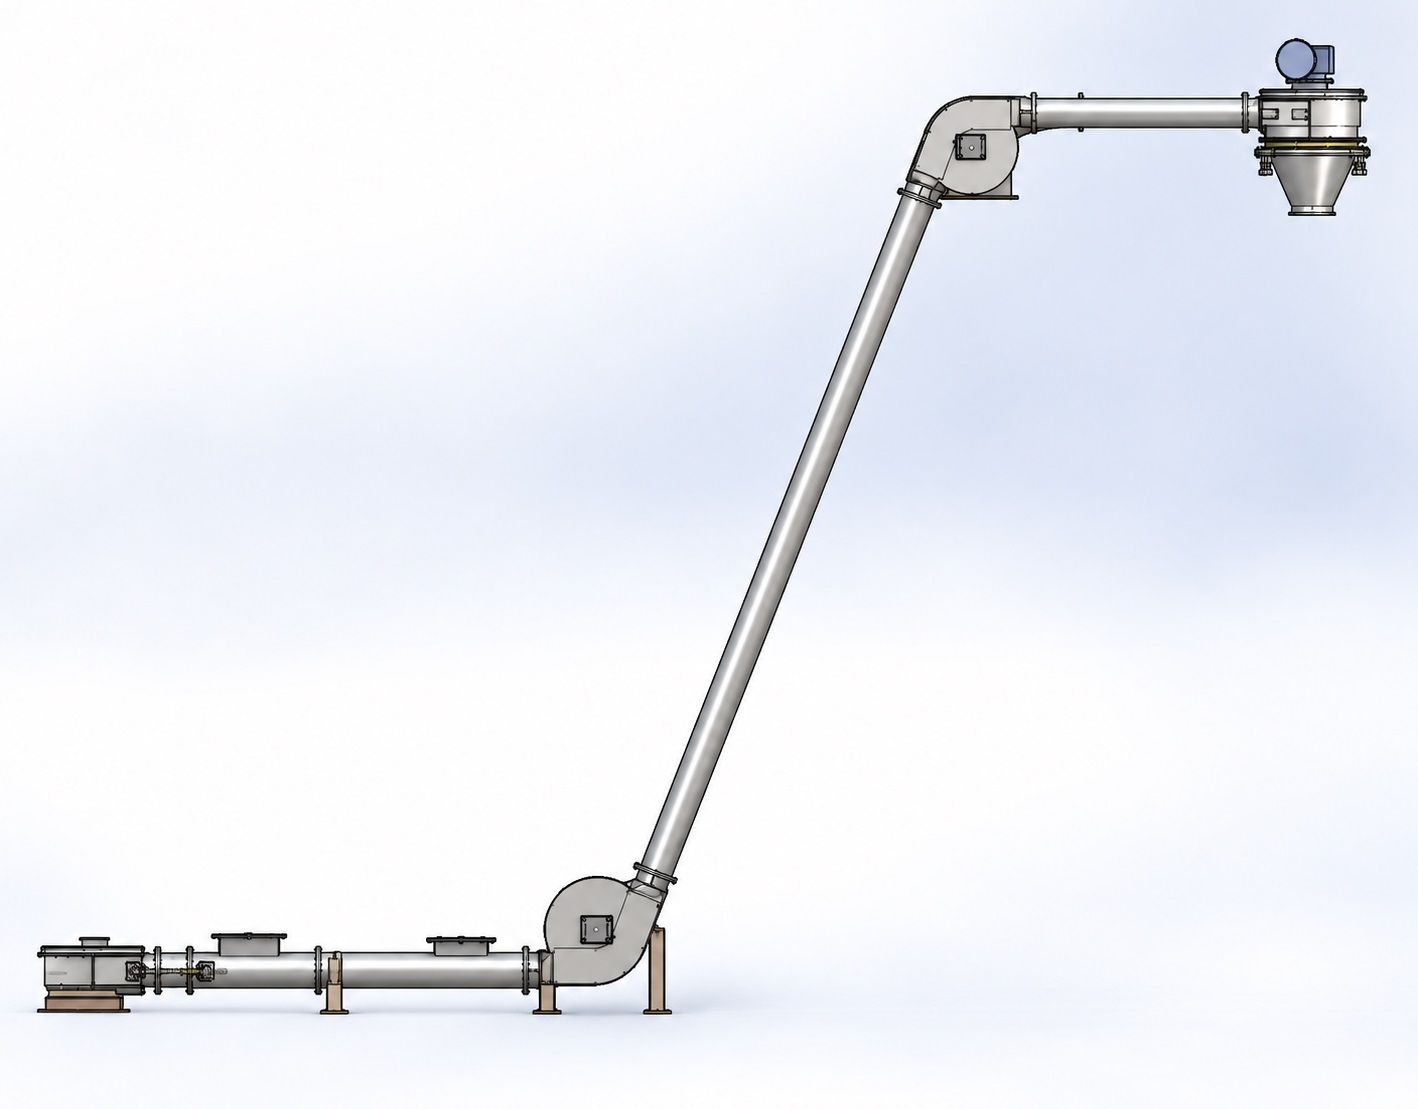
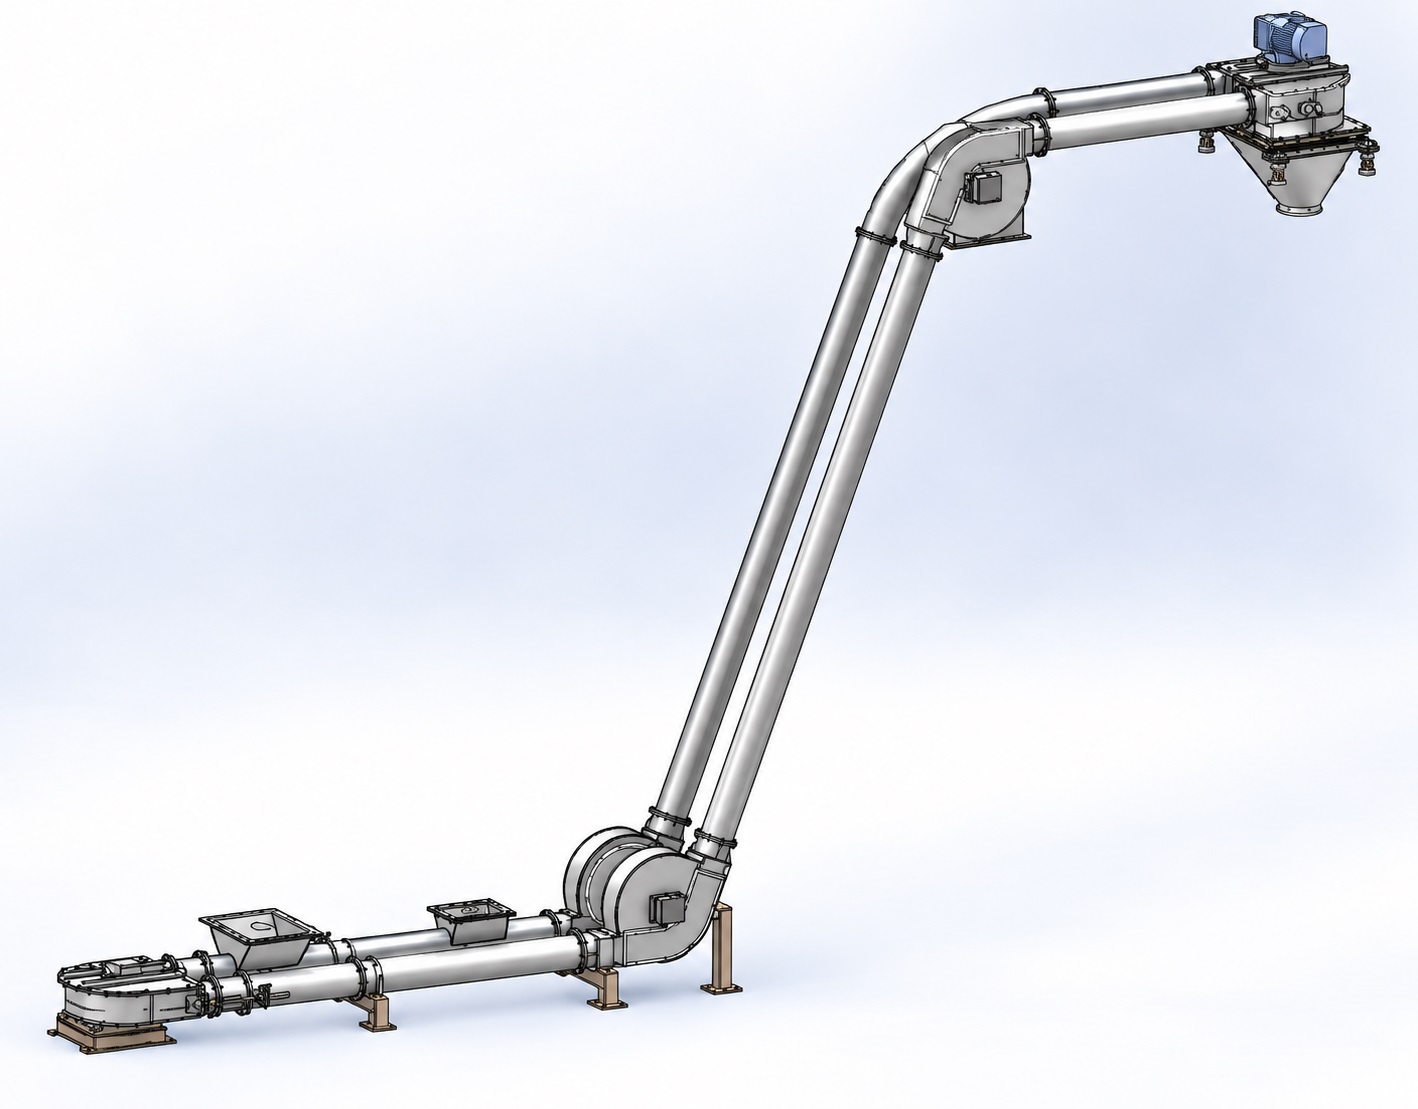
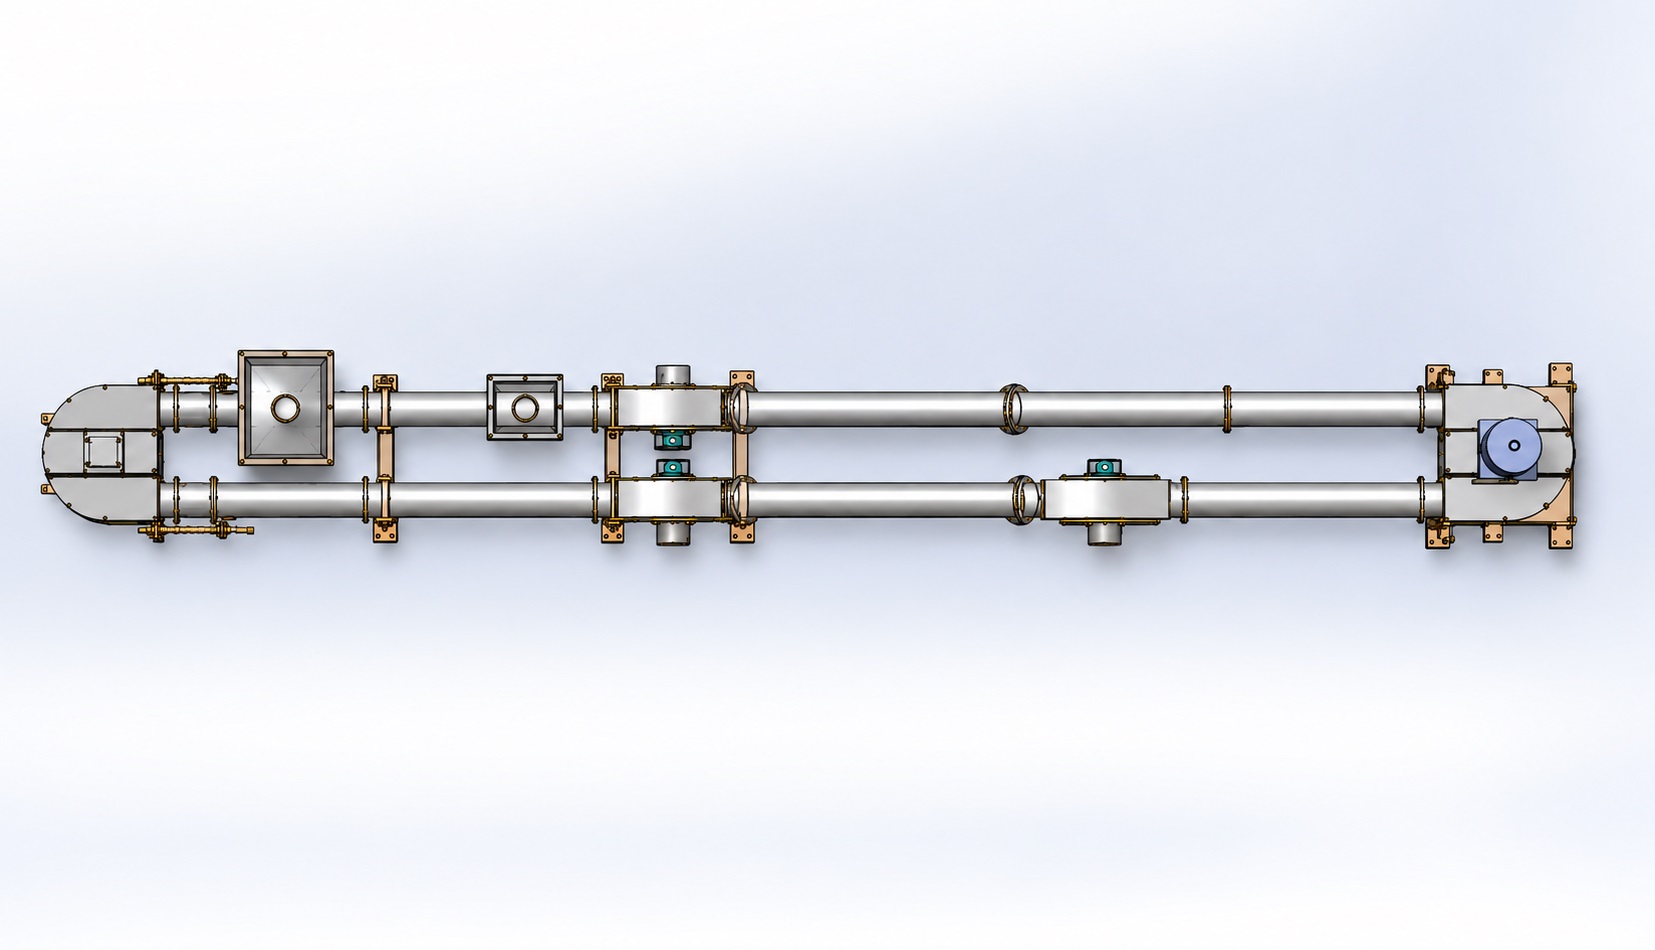
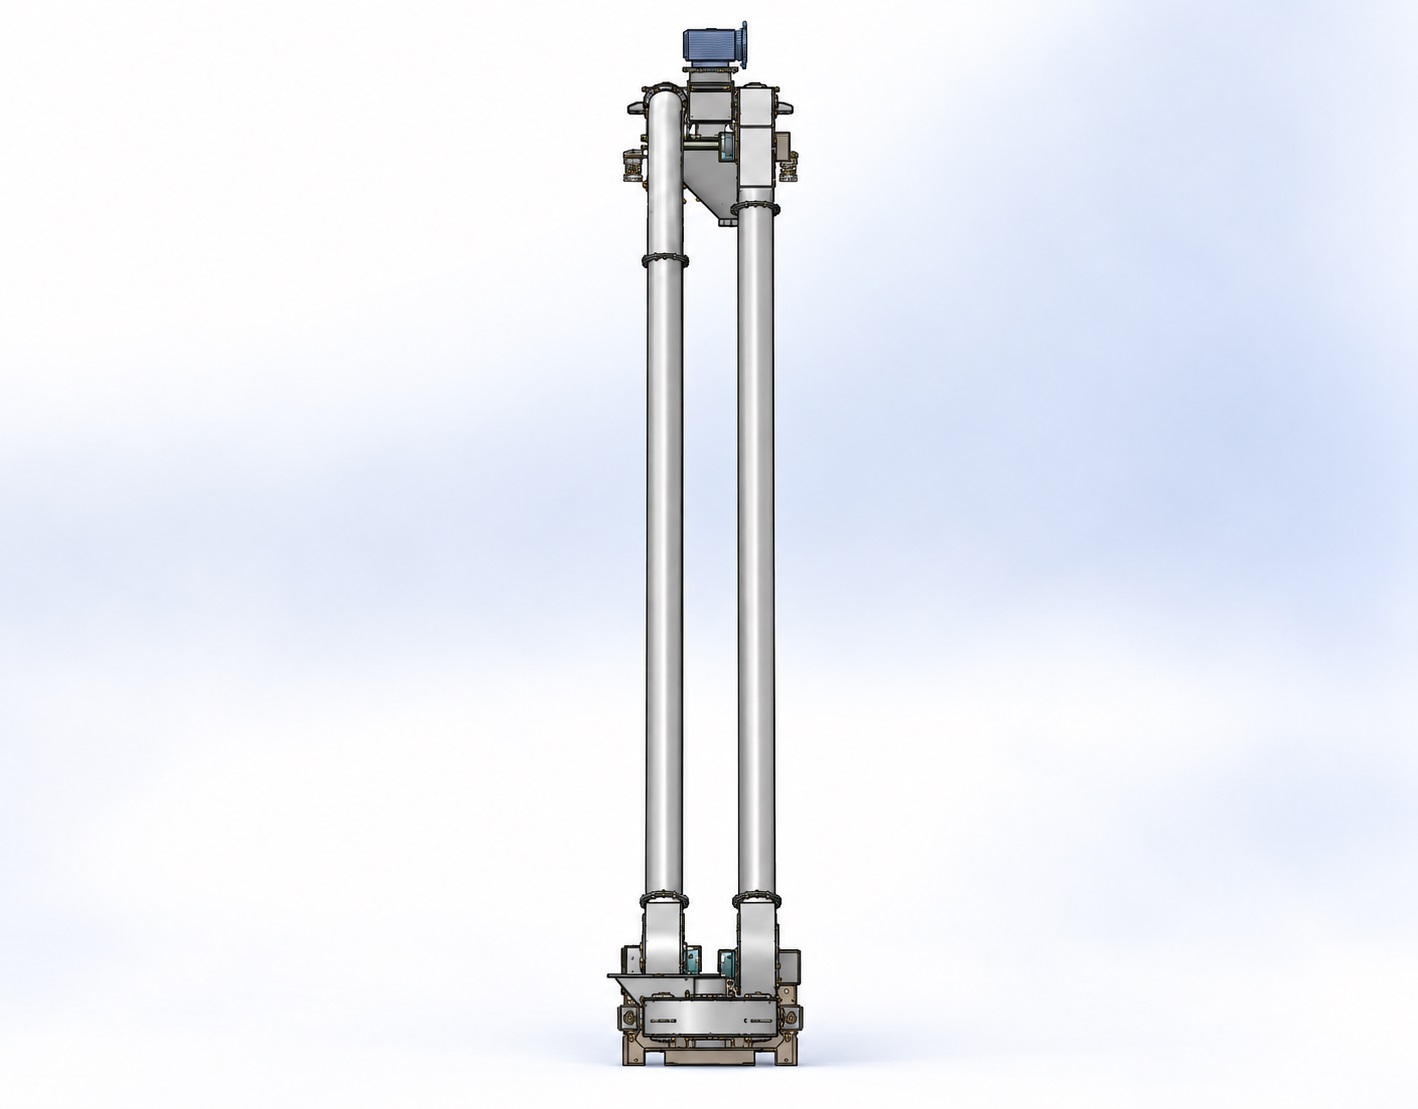
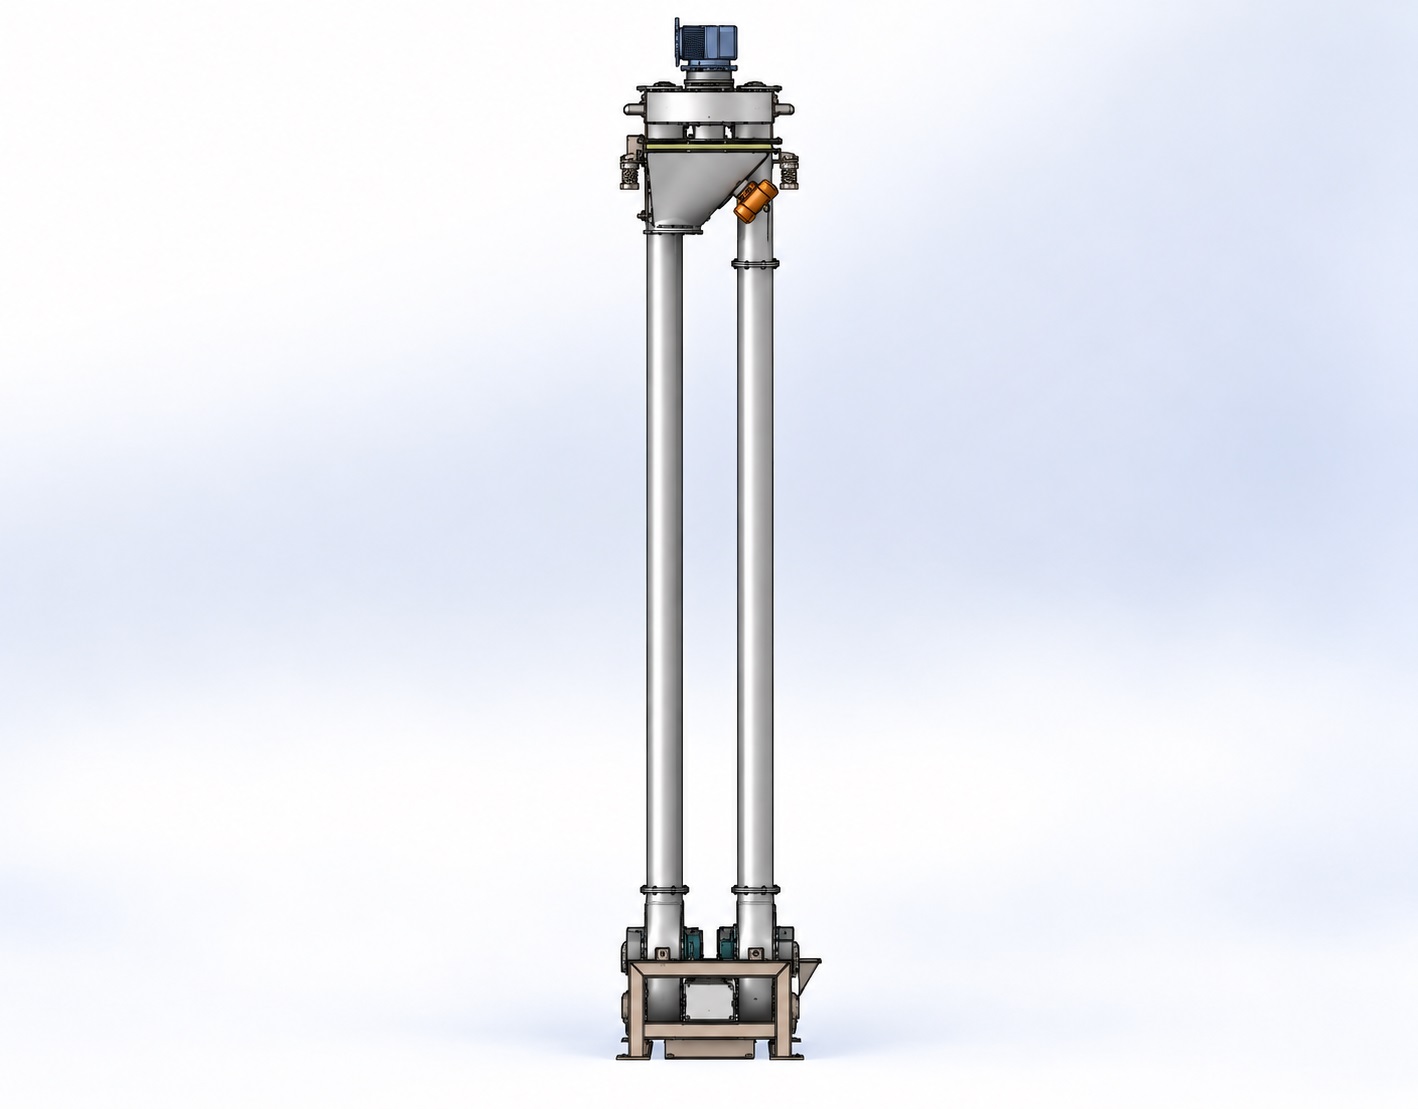
Engineered to navigate tight spaces with ease, tubular chain conveyors excel where traditional methods fall short. The conveyor drags material inside a totally enclosed casing, ensuring complete displacement and zero dust. It is extensively used for dry bulk solids, fly ash, and wet cake/materials with moisture content up to 5% to 10%. The system can be customized to suit any layout profile across X, Y, and Z planes.
Why Choose Raman Systems Pvt ltd
Raman Systems Pvt Ltd. stands out as the premier choice among Tube Chain Conveyor Manufacturers in Mumbai, delivering unmatched performance, reliability, and custom-tailored engineering support from consultation to installation and commissioning.
Recent Post
Get Our Latest Product
Catalogue & Updates
Subscribe to receive our latest industrial catalogues, automation solutions, and technical brochures directly in your inbox.